

 FCI
 SmartMeasurement
 ICEMECA
 SETNAG
 FLS
 KROHNE


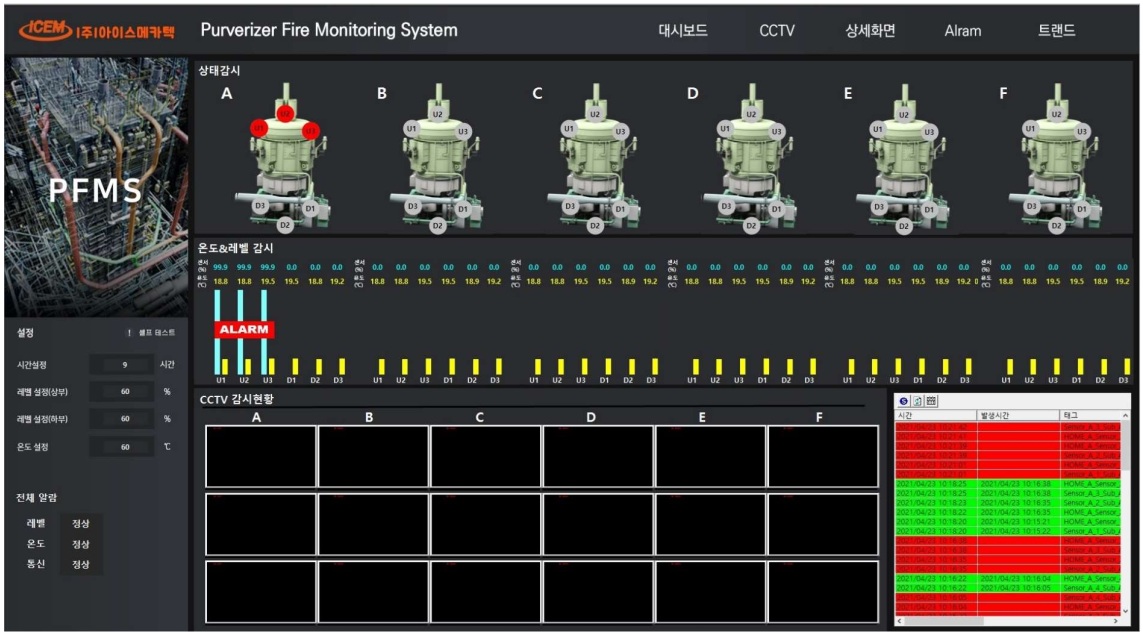
The Pulverizer Fire Monitoring System is an advanced safety solution designed to enhance the operational safety of coal-fired power plants. This system utilizes cutting-edge technology, including Infrared (IR) sensors and specialized cameras, to monitor and detect potential fire and explosion hazards within pulverizers.
-
Key Benefits
Enhanced Safety
– Early detection of fire risks significantly reduces the likelihood of catastrophic events.
Operational Continuity
– Continuous monitoring minimizes downtime by allowing proactive maintenance.
Cost Efficiency
– Prevents expensive damage to equipment and reduces maintenance costs through early intervention.
Regulatory Compliance
– Meets stringent safety and environmental standards for coal-fired power plants.
The Pulverizer Fire Monitoring System represents a crucial advancement in the safety and operational management of coal-fired power plants. By integrating state-of-the-art IR sensors and special cameras, this system offers a reliable and efficient means of preventing fire and explosion incidents, thereby safeguarding both personnel and equipment.
To explore more about our Pulverizer Fire Monitoring System (PFMS), please click on the Youtube below for further videos in details:
